
Factory Modernization That Boosts Efficiency, Visibility, and Output
Introduction
The customer manufactures passive components such as resistors, capacitors, and inductors for a wide range of industries, including consumer electronics, communications, computing, and automotive manufacturing. To remain competitive, the company must maintain strict quality standards and ensure stable, efficient production processes.
Before implementing the solution, the production machines operated as standalone systems without network connectivity. Operators had to manually inspect each machine to monitor production status, a time-consuming process that reduced efficiency and delayed the detection of abnormal operating conditions.
The ICP DAS USA’s solution enables the customer to collect and centralize data from field equipment for real-time monitoring, data logging, analysis, management, and reporting. As a result, the company gained a comprehensive production monitoring system that improves visibility, operational efficiency, and production line performance.
Machine Data Monitoring Solution: Temperature and Equipment Status Tracking
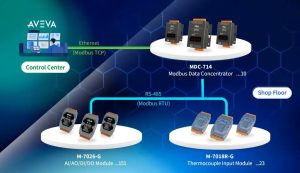
In this application, the customer deployed 151 M-7026-G Multi-function I/O Modules and 23 M-7018R-G Thermocouple Input Modules to collect temperature and operating status data from 120 production machines. The data is aggregated by MDC-714 Modbus Data Concentrators and transmitted to the control center for monitoring and analysis.
At the control center, AVEVA Edge HMI/SCADA software provides real-time visualization, data logging, trend analysis, alarm management, and historical reporting. The software automatically calculates upper and lower control limits, generates trend charts, issues alarms when abnormal conditions occur, and stores operational data for future analysis.
Because of the large production area, the customer deployed 10 MDC-714 Modbus Data Concentrators to support centralized monitoring and simplify system management. This distributed architecture also enhances system reliability by helping maintain operations even if the host computer or an individual data concentrator experiences a failure.
The system architecture is shown below:
Solution Architecture and System Operation
The solution combines ICP DAS USA’s I/O modules, Modbus data concentrators, and AVEVA Edge HMI/SCADA software to provide centralized monitoring, data analysis, and alarm management across the production facility.
M-7026-G multi-function I/O Module
The M-7026-G multi-function I/O Module features:
Each analog input channel can be configured independently, while the digital outputs can be used for alarm activation and control functions.
In this application, the M-7026-G collects machine energy consumption and operational data, including:
The collected data is sent to the MDC-714 Modbus Data Concentrator for aggregation and then transmitted to AVEVA Edge for monitoring and analysis.
M-7018R-G Thermocouple Input Module
The M-7018R-G Thermocouple Input Module provides 8 analog input channels and supports current, voltage, and thermocouple measurements. It also includes open thermocouple detection, enabling maintenance personnel to quickly identify sensor failures or wiring issues.
Each production machine in this application contains three heating rods. If any heating rod malfunctions, an entire production batch may be compromised. Traditional monitoring methods may miss these issues when temperatures remain within acceptable limits, even though a heating rod is operating abnormally.
To address this challenge, the M-7018R-G continuously collects temperature data from each heating rod. AVEVA Edge then applies temperature differential algorithms to compare readings and identify abnormal deviations. When temperature differences exceed predefined thresholds, operators are immediately notified, allowing corrective action before product quality is affected.
MDC-714 Modbus Data Concentrator
The MDC-714 Modbus Data Concentrator, part of the MDC-700 Series, bridges Modbus RTU and Modbus TCP networks through RS-232, RS-485, and Ethernet connectivity.
Rather than polling each device individually, the MDC-714:
In this deployment, the MDC-714 gathers Modbus RTU data from the M-7026-G and M-7018R-G modules and transmits the consolidated information to the host computer using Modbus TCP.
Because the facility spans multiple buildings and production areas, the customer installed 10 MDC-714 units throughout the plant. This distributed architecture simplifies data collection, improves scalability, and enhances reliability by preventing a single device failure from impacting the entire monitoring system.
AVEVA Edge HMI/SCADA Software
AVEVA Edge serves as the central monitoring and analysis platform, providing:
Using the data collected from the production floor, AVEVA Edge automatically:
Furnace Performance Comparison
To improve process consistency, AVEVA Edge allows operators to overlay data from multiple production runs and furnaces.
By comparing production trends and process parameters, personnel can:
This capability helps improve production yield, product quality, and manufacturing efficiency.
Heating Rod Temperature Differential Monitoring
In addition to traditional alarm thresholds, AVEVA Edge calculates temperature differences between heating rods.
The system continuously monitors:
When the temperature differential exceeds a predefined threshold, an alarm is triggered even if individual temperature readings remain within acceptable operating limits. This proactive approach helps detect hidden equipment issues and prevents material waste caused by undetected heating rod failures.
Real-Time Production Visibility
AVEVA Edge provides real-time visibility into:
As a result, operators can monitor the entire production line from a central location without performing time-consuming manual inspections.
Key Benefits
Reliable and Flexible I/O Data Collection
The M-7000 Series Remote I/O Modules support both Modbus RTU and DCON protocols and provide a wide range of analog and digital I/O options for monitoring current, voltage, temperature, and other process variables.
Advanced reliability features include:
These capabilities improve system availability and operational reliability.
Rugged Temperature Monitoring
The M-7018R-G offers industrial-grade protection, including:
These protections make the module ideal for harsh industrial environments.
Simplified Data Integration
The MDC-700 Series supports:
A built-in web server enables easy configuration, monitoring, and maintenance through a standard web browser without requiring additional software.
Faster Configuration and Maintenance
The MDC-700 Series supports CSV-based configuration files, allowing users to:
Optional Enhancement: WISE Edge Controller
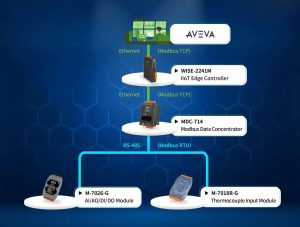
For even greater intelligence and system resilience, the customer can deploy a WISE-2241M IIoT Edge Controller.
The WISE Edge Controller offers:
Its built-in data logger includes automatic data recovery. If communication is interrupted, data continues to be stored locally and is automatically synchronized with the control system once connectivity is restored.
By offloading processing tasks from the host PC, the WISE-2241M further improves system scalability, reliability, and operational visibility across the production facility.
Conclusion
The ICP DAS Machine Temperature and Status Monitoring Solution enabled the customer to connect and centrally monitor 120 production machines, providing real-time visibility into equipment status, temperature, and production performance.
By combining intelligent data acquisition, centralized monitoring, trend analysis, and automated alarms, the solution helps operators quickly identify abnormalities, reduce downtime, improve production efficiency, and maintain consistent product quality.
This project highlights how ICP DAS solutions help manufacturers transform isolated equipment into connected, data-driven operations, laying the foundation for smarter, more efficient factories.


